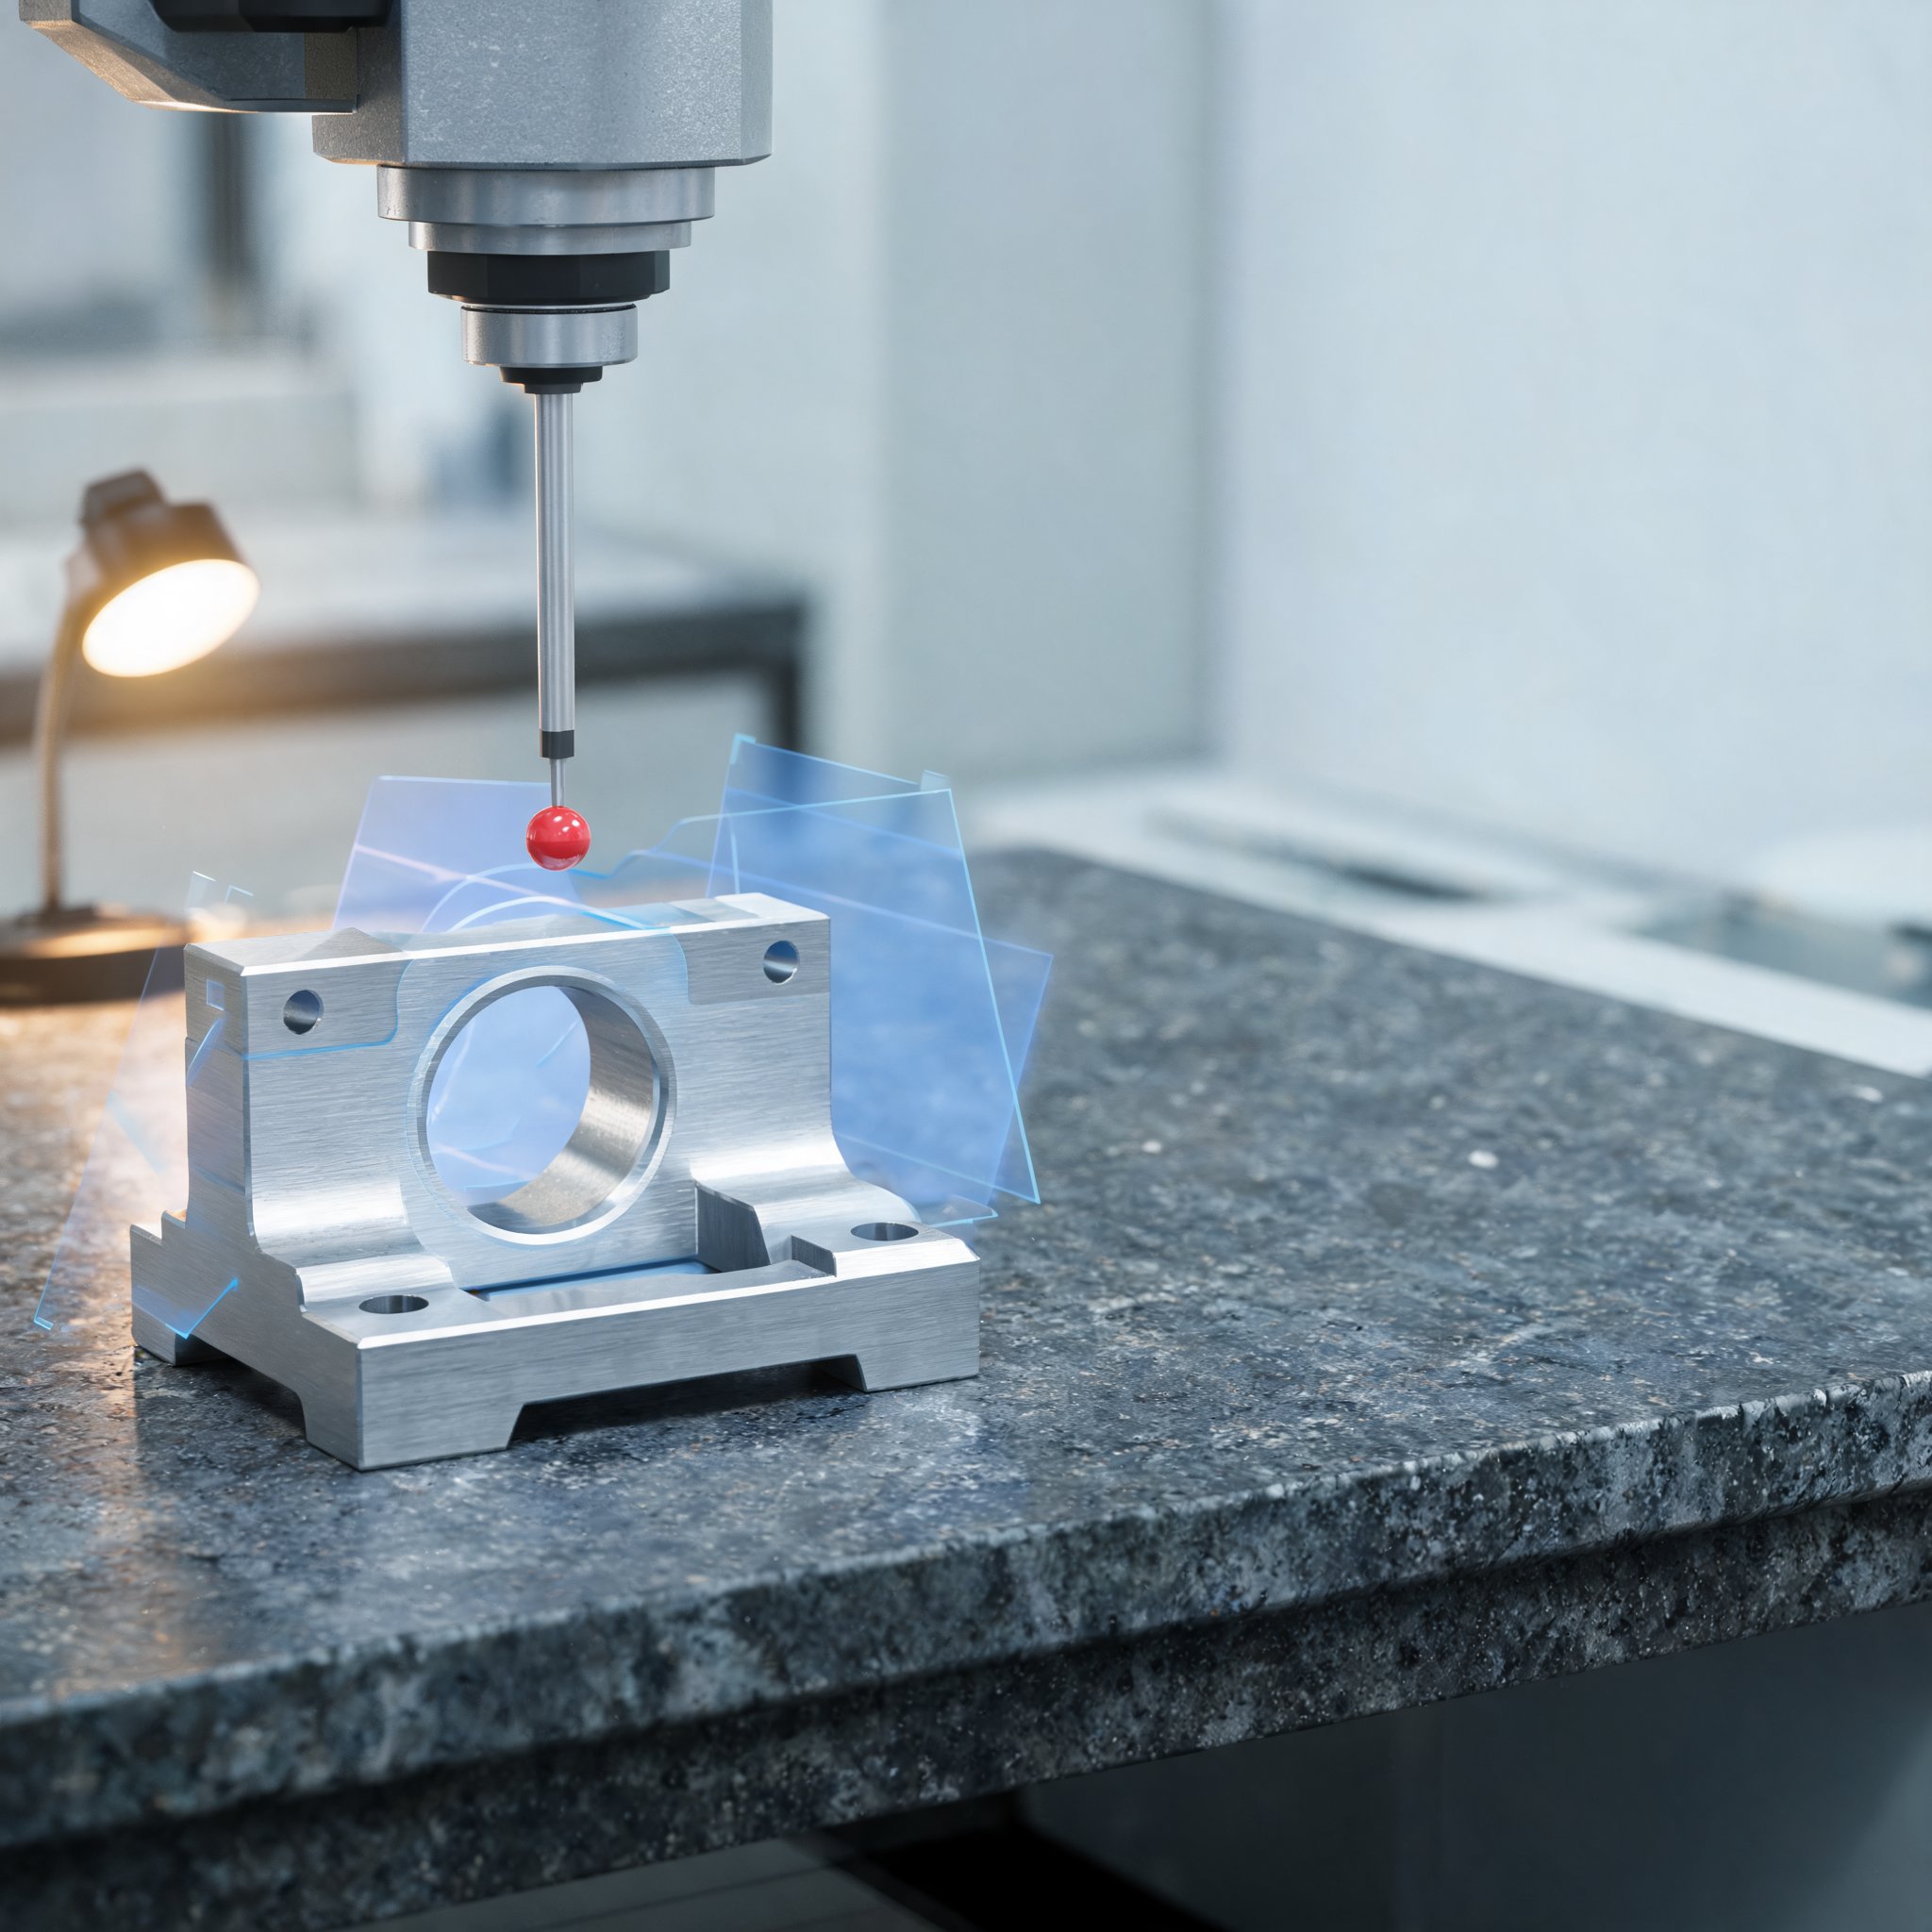
Metrologic DCS has set out four recommendations for narrowing the gap between design intent and what is actually measured on the shop floor, framing geometric dimensioning and tolerancing (GD&T) as the language that connects design, production and metrology. Used well, the company says, GD&T helps ensure a part assembles and functions as intended; misinterpreted, it produces conflicting measurements, scrap and costly back-and-forth between teams.
The company notes that product manufacturing information (PMI) is increasingly embedded in CAD files while standards continue to evolve, which it says multiplies the opportunities for error. Its four tips run from reading design intent through to the reports handed to machine operators.
Start from the PMI
Using PMI requires decoding the design intent: which feature is targeted, which references apply and which tolerance is specified. Metrologic DCS says manual handling at this stage is error-prone, since a value copied incorrectly or a reference misunderstood leads to a part being inspected against a requirement that was never specified. Its advice is to use software that takes the PMI as its starting point rather than re-entering tolerances, so that features and their evaluations are created from the part's digital definition. The company says the result is no re-keying, fewer interpretation gaps and time saved from the first step of program preparation.
Do not rebuild datum reference frames by hand
The datum reference frame (DRF) establishes where measurement starts. It is built from reference features A, B and C and determines which of the part's degrees of freedom are constrained for the evaluation. Metrologic DCS warns that building it in the wrong order, or selecting degrees of freedom poorly, can leave the same part declared conforming or non-conforming depending on the operator, which it describes as a major source of GD&T misinterpretation. It recommends automating the step so the DRF and its degrees of freedom follow from the drawing definition rather than operator choice, making results repeatable from one operator, machine and site to the next. In its Metrolog software, the company says, the DRF is created automatically when a GD&T is evaluated.
Reuse imported DRFs to limit rework
References A, B and C already carry labels placed by the design office in the CAD model. Recreating them during program preparation wastes time, opens the door to discrepancies and forces rework whenever the definition changes, the company says; on a part with many annotations it is also hard to know which ones have been handled and which remain to be measured. Its advice is to start from the DRFs coming from the PMI and predefine GD&T from them, while keeping a clear view of where each annotation sits on the part and where its measurement stands. In Metrolog, a function named Scan GDT reads the decoded PMI and assigns a status so both the decoding and the measurement can be validated.
Make reports useful to their reader
A report limited to pass or fail does not tell the shop floor what to do, according to Metrologic DCS: an operator who does not know which kind of defect they are dealing with adjusts by trial and error, producing scrap and correction loops. The company recommends tailoring the report to its reader — a table of numerical values for quality control, a go/no-go report for a quick decision, and a decomposition analysis for the operator. Metrolog splits the defect of an evaluated feature into four independent types (form, size, position and orientation) alongside the global defect, so the dominant type is visible and the first correction can be prioritised. The company says a good report reduces scrap and speeds corrective action.